


This article examines the most common performance problems affecting yogur congelado makers and provides practical, third-person solutions for operators, technicians, and business owners. It begins by explaining how frozen yogurt machines work and identifying key performance indicators such as draw temperature, overrun, freeze-down time, and recovery time. It then explores ten frequent issues: soft or inconsistent texture, long freezing times, motor stalling or overheating, excessive noise or vibration, leaking or overflowing, dasher or paddle failure, frost build-up or ice crystals, mid-cycle stops, cleaning difficulties, and inconsistent batch results. Each problem is analyzed with root causes and step-by-step remedies. The article includes a diagnostic table, preventive maintenance best practices, advanced troubleshooting for refrigeration, control systems, and drive systems, as well as guidance on mix pumps, hygiene, energy efficiency, staff training, and seasonal considerations. A preventive maintenance schedule is provided, along with case examples that illustrate real-world troubleshooting. The article also discusses when to repair, replace, or upgrade a machine, and it highlights the importance of choosing a reliable manufacturer. It mentions Jiangmen Taifai Technology Co.,Ltd, also known as TAIFAI, a high-tech kitchen appliance manufacturer founded in 2007 in Jiangmen City, Guangdong Province, China. TAIFAI supports OEM, ODM, and CKD projects, holds 50 patents, owns 50 moulds, follows ISO9001:2015, and offers products with CE, CB, GS, and RoHS certification. The conclusion emphasizes that a holistic approach combining correct mix formulation, proper pre-chilling, regular cleaning, and professional maintenance can ensure consistent, high-quality frozen yogurt and minimize downtime.
Yogur congelado makers, also known as frozen yogurt machines, have become essential equipment in dessert shops, restaurants, cafes, and even modern households. When these machines perform well, they deliver smooth, creamy, and consistently frozen yogurt that delights customers and satisfies family members. When they perform poorly, the results can range from soft, soupy product to noisy operation, motor failure, leaks, and costly downtime. Solving performance problems requires a systematic approach that examines ingredients, machine assembly, maintenance, environmental conditions, and the mechanical and electrical design of the equipment itself. This article explores the most common performance issues associated with yogur congelado makers and provides detailed, practical solutions for operators, technicians, and business owners.
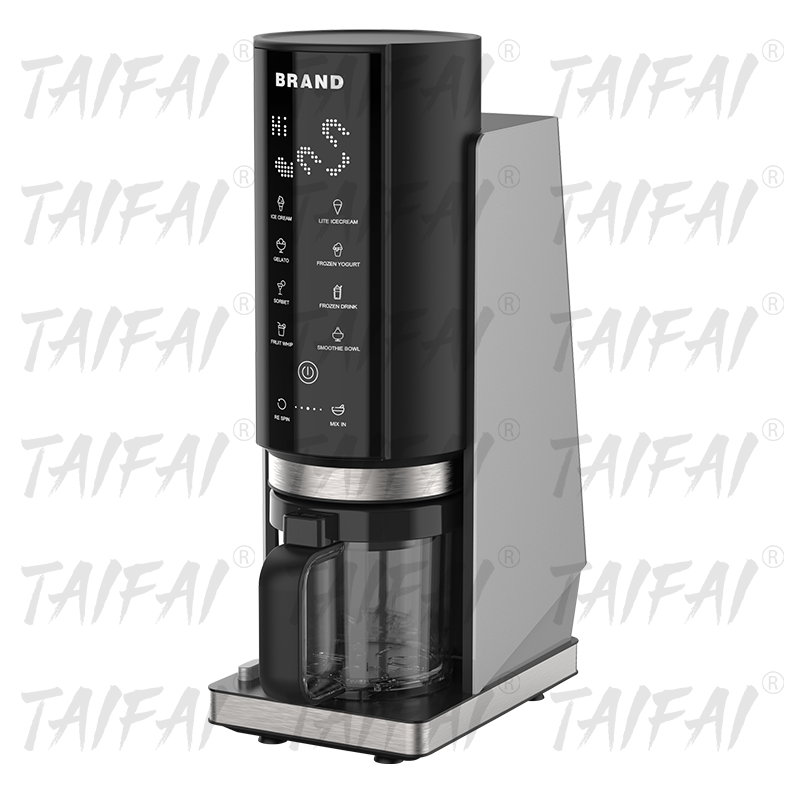
A yogur congelado maker is a specialized appliance that combines a refrigeration system, a mixing mechanism, and a control system. The refrigeration system cools the mixture, the dasher or auger scrapes the frozen product from the cylinder wall, and the control system regulates temperature, consistency, and timing. The quality of the final product depends on the interaction of these components. If any part is misadjusted, dirty, worn, or improperly used, performance suffers. Therefore, troubleshooting should begin with a clear understanding of how the machine is supposed to work.
undefined
Most commercial frozen yogurt machines use a cylindrical freezing chamber surrounded by evaporator coils. A compressor circulates refrigerant, absorbing heat from the mixture. A dasher rotates inside the cylinder, scraping frozen yogurt from the walls and incorporating air. The beater or auger also pushes product toward the dispensing spout. The control board monitors temperature and sometimes torque, adjusting the compressor and motor to maintain the desired consistency. Household models may use a pre-frozen bowl or a thermoelectric cooling system, but the principles remain similar: remove heat, agitate the mixture, and dispense at the right texture.
Operators should evaluate performance using measurable indicators. These include draw temperature, overrun, texture, freeze-down time, recovery time, noise level, power consumption, and leakage. Draw temperature is the temperature of the product as it leaves the spout. Overrun is the amount of air incorporated into the product, expressed as a percentage. Freeze-down time is how long the machine takes to bring the mix from a liquid state to a servable consistency. Recovery time is how quickly the machine returns to the correct consistency after dispensing. When any of these indicators fall outside the expected range, a performance problem exists.
Performance problems rarely have a single cause. They usually result from a combination of operational errors, maintenance neglect, and environmental factors. The following sections examine the most frequent complaints and provide step-by-step solutions.
Soft product is the most common complaint. The yogurt may dispense as a liquid, or it may be firm at first and then collapse. The root causes include incorrect mix formulation, insufficient pre-chilling, warm ambient temperature, worn dasher blades, low refrigerant charge, dirty condenser coils, faulty temperature sensors, and improper machine settings. The operator should first check the mix ratio. Too much water, alcohol, or sugar can lower the freezing point. Too much fat can also interfere with freezing if the mix is not homogenized. The operator should use a recipe designed for the specific machine and follow the manufacturer's recommendations.
Next, the operator should verify that the mix is pre-chilled to the recommended temperature, usually between 2 degrees Celsius and 4 degrees Celsius (35 degrees Fahrenheit and 39 degrees Fahrenheit). If the mix is warm, the machine must work harder and longer, and it may never reach the correct consistency during busy periods. Ambient temperature also matters. A machine placed near an oven, direct sunlight, or a heating vent will struggle. The operator should maintain an ambient temperature below 25 degrees Celsius (77 degrees Fahrenheit) and ensure adequate ventilation around the machine.
Mechanical causes require technician attention. Worn dasher blades reduce scraping efficiency, leaving frozen product on the cylinder wall and resulting in uneven texture. A low refrigerant charge reduces cooling capacity. Dirty condenser coils restrict heat rejection. A faulty temperature sensor can cause the control board to misread the product temperature. The technician should check the refrigerant pressure, clean the condenser, test the sensor, and replace worn blades. In some cases, the machine may need a software recalibration or a firmware update.
Long freezing times frustrate operators during peak hours. The machine may take 30 minutes or more to freeze a batch that should take 10 to 15 minutes. Causes include a warm mix, a warm cylinder, a dirty condenser, a failing compressor, a restricted capillary tube, a faulty fan motor, or a machine that is simply too small for the production volume. The operator should pre-chill the mix and the cylinder. Some machines have a standby mode that keeps the cylinder cold. If the machine has been off for hours, the operator should run it in standby or freeze mode before adding mix.
If the mix and cylinder are cold, the technician should inspect the refrigeration system. A dirty condenser is a frequent culprit. The technician should clean the coils with a soft brush and coil cleaner. The fan motor should spin freely and move air across the coils. If the compressor is hot, noisy, or drawing high current, it may be failing. A restricted capillary tube or expansion valve can reduce refrigerant flow. The technician should check pressures and temperatures to diagnose the issue. In some cases, the machine may be undersized. If the shop regularly sells more than the machine can produce, the owner should consider a larger or additional machine.
The motor that drives the dasher can stall or overheat when the product becomes too hard, when the mix is too thick, when the dasher is misaligned, or when the motor is worn. A stalled motor may hum but not turn, or it may trip a thermal overload. The operator should never force a stalled machine. Instead, the operator should turn off the machine, allow it to warm up, and then investigate. If the product is too hard, the operator should adjust the consistency setting or the mix formulation. If the dasher is misaligned, the technician should realign it and check the drive belt or gearbox.
Overheating can also result from a lack of ventilation. The motor compartment must be free of dust and obstructions. The technician should clean the motor cooling fan and ensure that the machine has adequate clearance. If the motor continues to overheat, the technician should test the winding resistance and capacitor. A worn capacitor can cause the motor to draw excessive current. If the motor is mechanically seized, it may need replacement. Regular lubrication of the drive system, if applicable, can prevent premature wear.
Noise and vibration are not just annoyances; they often indicate mechanical problems. Common causes include loose panels, worn bearings, a damaged dasher, a bent drive shaft, a failing fan motor, a compressor that is failing, or a machine that is not level. The operator should first check that the machine is level and that all feet are firmly on the floor. Loose panels can be tightened. The operator should also check for foreign objects in the cylinder.
If the noise persists, the technician should inspect the bearings and drive shaft. Worn bearings can cause a grinding or rumbling sound. A bent drive shaft can cause vibration and uneven scraping. The technician should replace worn parts. The fan motor and compressor should also be checked. A compressor that is failing may produce a loud knock or rattle. In some cases, the noise may come from the refrigeration lines vibrating against the cabinet. The technician can adjust or insulate the lines to reduce noise.
Leaks can occur from the dispensing spout, the door seal, the cylinder gasket, or the drain tube. Overflowing usually results from overfilling the cylinder or using a mix that expands too much. The operator should never fill the cylinder above the recommended level. The operator should also check that the spout is fully closed and that the seals are clean and properly seated. A worn O-ring or gasket should be replaced. If the leak is from the refrigeration system, the technician should check for refrigerant oil stains and use an electronic leak detector.
Overflowing can also be caused by a blocked air vent or a faulty pressure relief valve. The technician should inspect the vent and valve. In some machines, the mix may foam excessively due to high protein content or improper mixing. The operator should allow the mix to hydrate properly and avoid over-whipping. If the machine has a mix pump, the technician should check the pump pressure and tubing.
If the dasher does not turn, the machine cannot produce proper frozen yogurt. Causes include a broken drive belt, a stripped gear, a faulty motor, a misaligned coupling, or a safety switch that is not engaged. The operator should first ensure that the machine is properly assembled and that the safety switch is activated. If the machine has a door interlock, the door must be fully closed. If the dasher still does not turn, the technician should inspect the drive system. A broken belt is easy to replace. A stripped gear or worn coupling may require more extensive repair.
In some cases, the dasher may be stuck because frozen product has built up around it. The operator should defrost the machine according to the manufacturer's instructions. Never use sharp tools to chip away ice, as this can damage the cylinder. After defrosting, the technician should check the dasher for damage and ensure that it rotates freely by hand before reassembling.
Frost build-up on the evaporator or in the cylinder can reduce efficiency and create icy texture. Causes include a faulty door seal, high humidity, frequent door openings, a defrost system failure, or a drain that is clogged. The operator should check the door seal and replace it if it is torn or brittle. The operator should also minimize door openings and ensure that the machine is not placed in a humid area. If the machine has an automatic defrost cycle, the technician should test the timer and heater.
Ice crystals in the product can result from slow freezing, insufficient agitation, or a mix with high water content. The operator should ensure that the dasher is turning at the correct speed and that the mix is properly formulated. Adding stabilizers or using a commercial mix can help. The technician should also check the refrigerant charge and the expansion valve, as these affect freezing speed.
A machine that stops mid-cycle may be experiencing a thermal overload, a power supply issue, a faulty control board, a sensor error, or a safety trip. The operator should check the power cord, outlet, and circuit breaker. If the machine shares a circuit with other high-power equipment, it may not receive enough voltage. The operator should plug the machine into a dedicated circuit. If the machine has an error code, the operator should consult the manual.
The technician should test the motor overload, the compressor overload, and the control board. A dirty condenser can cause the compressor to overheat and trip. A faulty sensor can send incorrect signals to the board. The technician should test all sensors and replace any that are out of specification. If the control board is faulty, it may need to be replaced or reprogrammed.
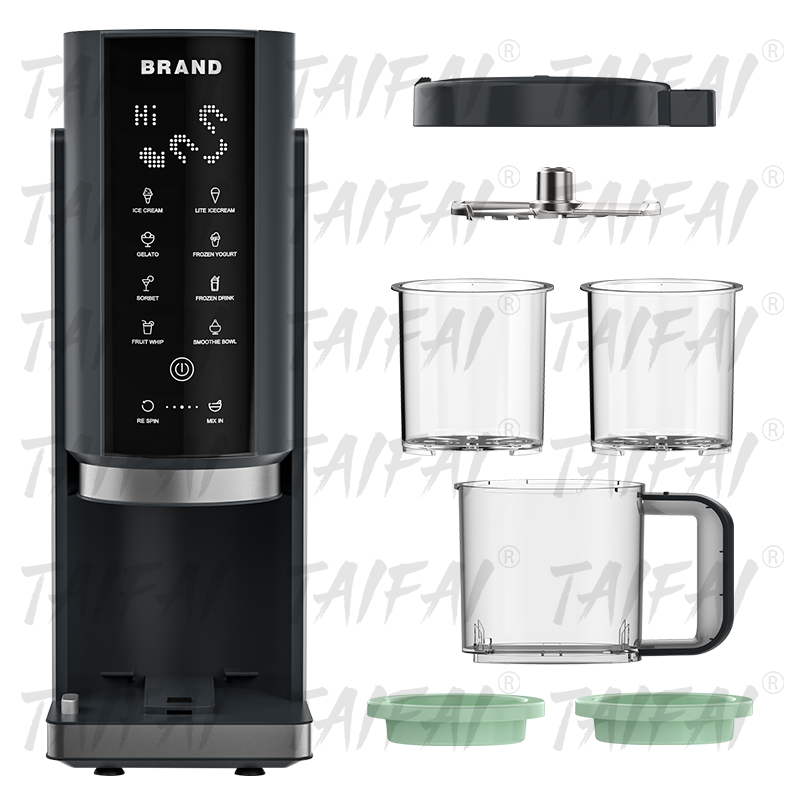
Cleaning is critical for food safety and performance. If the machine is difficult to clean, residue can build up, causing odors, bacterial growth, and poor texture. The operator should disassemble all removable parts, including the dasher, spout, gaskets, and drip tray. These parts should be washed with warm water and a food-safe detergent, then sanitized according to local regulations. The operator should never use abrasive cleaners or sharp tools on the cylinder or dasher.
Some machines have automatic cleaning cycles. The operator should follow the manufacturer's instructions for these cycles. If the machine has hard-to-reach areas, the technician may need to remove panels or use a specialized cleaning tool. Regular cleaning prevents many performance problems, including leaks, motor overload, and off-flavors.
Inconsistent results can be frustrating. One batch may be perfect, while the next is too soft or too hard. Causes include inconsistent mix formulation, varying mix temperatures, fluctuating ambient conditions, worn components, and operator error. The operator should standardize the process. This includes weighing ingredients, using a calibrated thermometer, pre-chilling the mix, and following the same assembly and start-up procedure every time. The operator should also record draw temperatures and freeze-down times to identify trends.
If the process is consistent but results still vary, the technician should inspect the machine for worn parts. A worn dasher, a weak motor, or a refrigerant leak can cause gradual changes. The technician should perform a complete diagnostic and replace any components that are out of specification.
| Symptom | Likely Cause | Solution |
|---|---|---|
| Soft product | Warm mix, low refrigerant, worn dasher, wrong setting | Pre-chill mix, recharge refrigerant, replace dasher, adjust setting |
| Long freeze time | Dirty condenser, warm cylinder, undersized machine | Clean condenser, run standby, upgrade machine |
| Motor stalls | Hard product, misaligned dasher, worn motor | Adjust consistency, realign dasher, replace motor |
| Noise and vibration | Loose panels, worn bearings, bent shaft | Tighten panels, replace bearings, replace shaft |
| Leaking | Worn gasket, overfilled cylinder, loose spout | Replace gasket, reduce fill level, tighten spout |
| Dasher not turning | Broken belt, stripped gear, safety switch | Replace belt, replace gear, engage switch |
| Frost build-up | Bad door seal, high humidity, defrost failure | Replace seal, reduce humidity, repair defrost |
| Stops mid-cycle | Overload, power issue, faulty board | Check power, clean condenser, replace board |
Prevention is always better than repair. A well-maintained yogur congelado maker will perform better, last longer, and produce more consistent product. The following best practices should be part of every operator's routine.
The mix formulation has a direct impact on freezing performance. High sugar content lowers the freezing point, resulting in softer product. High fat content can create a richer texture but may also slow freezing. High water content can create ice crystals. Stabilizers and emulsifiers help control texture and reduce ice crystal formation. The operator should use a recipe that has been tested with the specific machine. If the operator wants to create a custom recipe, they should start with a commercial base and make small adjustments. They should also measure ingredients by weight, not volume, to ensure consistency.
Alcohol should be used sparingly, as it significantly lowers the freezing point. If alcohol is added, the operator may need to lower the consistency setting or pre-freeze the mix more. The operator should also avoid adding acidic ingredients directly to the mix, as they can curdle dairy proteins. If fruit purees are used, they should be added according to the recipe, and the operator should account for their water and sugar content.
Pre-chilling the mix is one of the simplest ways to improve performance. The mix should be stored in a refrigerator at 2 degrees Celsius to 4 degrees Celsius (35 degrees Fahrenheit to 39 degrees Fahrenheit) for at least four hours before use. This allows the mix to hydrate and reduces the workload on the machine. The operator should also pre-chill the cylinder by running the machine in standby mode for 10 to 15 minutes before adding mix. In hot environments, the operator should use a pre-cooler or keep the mix in an insulated container.
Ambient conditions should be controlled. The machine should be placed away from heat sources, direct sunlight, and high humidity. The operator should ensure that the machine has at least 10 cm (4 inches) of clearance on all sides for ventilation. If the ambient temperature exceeds 30 degrees Celsius (86 degrees Fahrenheit), the machine may struggle to freeze the product. In such cases, the operator should use a larger machine or improve the air conditioning.
Proper assembly is critical. The operator should follow the manufacturer's instructions for assembling the dasher, cylinder, spout, and seals. All parts should be clean and in good condition. The operator should never force parts together. The spout should be fully closed before adding mix. The operator should fill the cylinder to the recommended level, usually no more than 80 percent full. Overfilling can cause overflow, motor strain, and poor freezing. After filling, the operator should start the machine and allow it to run until the desired consistency is reached.
The operator should also check the mix level regularly. If the machine has a hopper, the operator should keep it filled within the recommended range. Running the machine with too little mix can cause the dasher to scrape the cylinder wall and wear out the blades. Running with too much mix can cause overflow and motor overload.
Daily cleaning is essential. The operator should disassemble the machine after each use or at the end of the day, depending on the manufacturer's recommendations. All food-contact parts should be washed, rinsed, and sanitized. The operator should use a food-safe sanitizer and allow parts to air dry. The operator should not reassemble the machine while parts are wet, as water can cause freezing problems and bacterial growth. The machine exterior should be wiped down with a damp cloth. The condenser coils should be cleaned monthly or more often in dusty environments.
When the machine is not in use for an extended period, the operator should clean and dry all parts, disconnect the power, and cover the machine to prevent dust accumulation. The operator should also follow the manufacturer's storage instructions. If the machine will be exposed to freezing temperatures, the operator should drain all water lines to prevent damage.
Regular electrical and mechanical checks can prevent major failures. The technician should inspect the power cord, plug, and outlet for damage. The technician should test the voltage and ensure that the machine receives the correct power. The technician should check the motor current, capacitor, and overloads. The technician should also inspect the drive belt, gears, bearings, and couplings for wear. The technician should lubricate moving parts according to the manufacturer's schedule. The technician should check the refrigerant pressure and look for oil stains that indicate leaks. The technician should clean the condenser and check the fan motor. These checks should be performed at least quarterly, or more often in high-volume operations.
When basic troubleshooting does not solve the problem, the technician must examine the refrigeration system in detail. The refrigeration system is the heart of the yogur congelado maker. It consists of a compressor, condenser, expansion device, evaporator, and refrigerant lines. Each component can cause performance problems if it fails or is improperly maintained.
The compressor pumps refrigerant through the system. If the compressor is weak, the machine will not cool properly. Symptoms include long freeze times, soft product, and high head pressure. The technician should measure the compressor current and compare it to the nameplate rating. A compressor that draws low current may be low on refrigerant or have internal damage. A compressor that draws high current may be overheating or mechanically seized. The technician should also check the start relay and capacitor. A failed start capacitor can prevent the compressor from starting. If the compressor is faulty, it must be replaced by a qualified technician.
The condenser releases heat from the refrigerant. If it is dirty, airflow is restricted, and the refrigerant cannot condense properly. This leads to high head pressure, reduced cooling capacity, and compressor overheating. The technician should clean the condenser coils regularly. The evaporator absorbs heat from the mix. If it is frosted or dirty, heat transfer is reduced. The technician should check for frost build-up and defrost the system if necessary. The evaporator fan, if present, should be checked for proper operation.
The expansion device controls the flow of refrigerant into the evaporator. A restricted capillary tube or a faulty expansion valve can cause low suction pressure and poor cooling. The technician should check the temperature difference across the expansion device. If the restriction is severe, the technician may need to replace the capillary tube or expansion valve. This requires recovering the refrigerant, cutting and brazing new components, evacuating the system, and recharging with the correct amount of refrigerant.
Incorrect refrigerant charge is a common cause of performance problems. If the system is undercharged, the machine will not freeze properly. If it is overcharged, the compressor may overheat and the system may not cool efficiently. The technician should recover the refrigerant, evacuate the system, and recharge by weight according to the manufacturer's specifications. The technician should also check for leaks using an electronic leak detector or soap bubbles. All leaks must be repaired before recharging.
Modern yogur congelado makers rely on electronic control systems. These systems monitor temperature, motor current, and sometimes product consistency. A faulty sensor or control board can cause a wide range of performance problems, including soft product, hard product, motor stalling, and mid-cycle stops.
Temperature sensors, such as thermistors or RTDs, provide feedback to the control board. If a sensor is faulty, the board may think the product is colder or warmer than it actually is. The technician should test the sensor resistance at known temperatures and compare it to the manufacturer's chart. A sensor that is out of range should be replaced. The technician should also check the wiring and connectors for corrosion or loose connections.
The control board processes sensor inputs and controls the compressor, motor, and fans. If the board is faulty, the machine may not start, may run continuously, or may display error codes. The technician should check for visible damage, such as burnt components or loose connectors. If the board is suspected, the technician should test the output voltages to the compressor and motor. A faulty board should be replaced or reprogrammed by the manufacturer.
Safety switches prevent the machine from operating when the door is open or the dasher is not properly installed. If a safety switch is faulty, the machine may not start. The technician should test the switch continuity and replace it if necessary. The technician should also check the door interlock mechanism for alignment and wear.
The drive system transfers power from the motor to the dasher or auger. It includes belts, gears, couplings, and bearings. Problems in the drive system can cause noise, vibration, stalling, and poor scraping.
Some machines use belts to drive the dasher. A worn or loose belt can slip, causing the dasher to turn slowly or not at all. The technician should check belt tension and condition. A glazed or cracked belt should be replaced. The technician should also check the pulleys for alignment and wear.
Gear-driven machines use gears and couplings to transfer power. A stripped gear or worn coupling can cause the dasher to stop turning. The technician should inspect these parts for wear and replace them as needed. Proper lubrication is essential to prevent premature wear.
Bearings support the drive shaft and allow it to rotate smoothly. Worn bearings can cause noise, vibration, and shaft misalignment. The technician should replace worn bearings and inspect the seals for leaks. A leaking seal can allow mix to enter the drive system, causing contamination and corrosion.
Some commercial machines use a mix pump to transfer product from the hopper to the freezing cylinder. The pump also incorporates air, which affects overrun. If the pump is not working correctly, the product may be too dense or too soft. The technician should check the pump pressure, tubing, and valves. The operator should ensure that the mix is free of lumps and that the hopper is not empty. Air leaks in the suction line can cause poor aeration. The technician should tighten all fittings and replace damaged tubing.
Performance problems can also be caused by poor hygiene. Residue from previous batches can harbor bacteria, create off-flavors, and interfere with freezing. The operator should follow a strict cleaning and sanitizing schedule. All food-contact surfaces should be cleaned and sanitized before each use. The operator should use test strips to verify sanitizer concentration. The machine should be disassembled and cleaned thoroughly at least once a day, or more often if required by local regulations. The operator should also practice good personal hygiene and use clean utensils.
Energy costs can be significant for frozen yogurt machines, especially in high-volume operations. Poor performance often increases energy consumption. A dirty condenser, a low refrigerant charge, or a worn motor can cause the machine to run longer and use more electricity. The operator should maintain the machine properly to keep energy costs down. The owner should also consider upgrading to a more energy-efficient model. Modern machines may use variable-speed compressors, electronically commutated motors, and improved insulation. These features can reduce energy consumption while maintaining performance.
Many performance problems are caused by operator error. Proper training is essential. Staff should be trained on how to assemble the machine, how to prepare the mix, how to start and stop the machine, how to adjust consistency, and how to clean and sanitize. They should also know what to do when the machine malfunctions. A standard operating procedure should be written and posted near the machine. It should include step-by-step instructions, safety warnings, and a troubleshooting guide. Regular refresher training can help maintain performance and reduce downtime.
Environmental conditions change throughout the year. In summer, high ambient temperatures and humidity can make it harder for the machine to freeze product. The operator should adjust the mix formulation, pre-chill more aggressively, and ensure adequate ventilation. In winter, low humidity can cause static electricity, and low ambient temperatures can affect the machine's settings. The operator should monitor the machine and adjust as needed. If the machine is in a mobile unit or an outdoor kiosk, the operator should protect it from direct sun, rain, and extreme temperatures.
| Frequency | Task | Responsible Party |
|---|---|---|
| Daily | Clean and sanitize all food-contact parts; inspect seals and gaskets | Operator |
| Weekly | Clean condenser coils; check mix levels and tubing | Operator or Technician |
| Monthly | Inspect drive belt, gears, and bearings; test sensors | Technician |
| Quarterly | Check refrigerant pressure; test compressor current; lubricate moving parts | Technician |
| Annually | Perform complete overhaul; replace worn components; update firmware | Technician or Manufacturer |
Not every performance problem can be solved with maintenance. Sometimes repair is not cost-effective, or the machine is simply not suitable for the operation. The owner should consider repair if the problem is isolated and the machine is otherwise in good condition. For example, a worn gasket or a dirty condenser is a simple repair. The owner should consider replacement if the machine is old, inefficient, and requires frequent repairs. A new machine may be more energy-efficient, produce better product, and reduce downtime.
The owner should also consider upgrading if the machine is undersized. If the shop consistently runs out of product during peak hours, a larger machine or an additional machine may be necessary. Upgrading to a machine with better controls, automatic defrost, and improved energy efficiency can also reduce operating costs. The owner should calculate the total cost of ownership, including purchase price, energy consumption, maintenance, and downtime, before making a decision.
The best way to avoid performance problems is to choose a high-quality machine from a reputable manufacturer. A well-designed machine will have robust refrigeration components, a powerful and efficient motor, easy-to-clean parts, and reliable controls. It will also come with clear instructions, spare parts availability, and technical support. When evaluating a supplier, buyers should consider manufacturing experience, quality certifications, production capacity, and customization options.
One example of a manufacturer with these qualities is Jiangmen Taifai Technology Co.,Ltd, also known as TAIFAI. Located in Jiangmen City, Guangdong Province, China, a flourishing home appliances manufacturing base, TAIFAI was founded in 2007. It is a high-tech enterprise with capabilities and services of independent research and development, production, and sales. The company's main products include electric blender, juicer, citrus juicer, hand mixer, hand blender, stand mixer, coffee grinder, chopper, and food processor. TAIFAI supports OEM, ODM, and CKD projects. The company holds 50 patents and owns 50 moulds. Its production of goods follows ISO9001:2015 standard, and it insists on strict management of production operation and quality. A variety of products have CE, CB, GS, and RoHS certification with fantastic design, good performance, multi-functional features, and reasonable price.
TAIFAI focuses on the manufacturing and service of kitchen electric appliances. It is a professional kitchen appliances manufacturer with excellent scale and technology in China. TAIFAI is a high-quality kitchen electric appliances provider integrating design, research, development, production, sales, and service. For businesses seeking a yogur congelado maker or other kitchen appliances, partnering with an experienced manufacturer like TAIFAI can help ensure reliable performance and long-term satisfaction.
A cafe reported that its frozen yogurt was consistently soft during the lunch rush. The operator had been using a mix that was stored at room temperature and added directly to the machine. The ambient temperature in the cafe was 28 degrees Celsius (82 degrees Fahrenheit). The technician recommended pre-chilling the mix to 3 degrees Celsius (37 degrees Fahrenheit) and running the machine in standby mode before the rush. The operator also adjusted the consistency setting to a firmer level. After these changes, the product texture improved significantly, and the machine recovered faster between servings.
A dessert shop reported that its machine motor stalled after a few minutes of operation. The operator had been using a thick, high-fat mix and had set the consistency to the maximum. The motor was also covered in dust. The technician cleaned the motor compartment, reduced the consistency setting, and advised the operator to use a mix with a lower fat content. The motor no longer stalled, and the machine ran smoothly.
A restaurant reported that its machine leaked from the spout. The operator had been overfilling the cylinder and had not replaced the spout O-ring in over a year. The technician replaced the O-ring, cleaned the spout, and instructed the operator to fill the cylinder only to the recommended level. The leak stopped, and the machine operated normally.
A high-volume frozen yogurt shop reported that product texture varied throughout the day. The operator was using the same mix but did not pre-chill it consistently. The shop also had the machine near a large window with direct afternoon sun. The technician recommended pre-chilling the mix to 3 degrees Celsius, moving the machine away from the window, and installing a small air conditioner to keep the ambient temperature below 25 degrees Celsius. The operator also began recording draw temperatures every hour. After these changes, texture became consistent, and customer complaints dropped.
A small kiosk reported that its machine stopped mid-cycle several times a day. The machine was plugged into an extension cord shared with a refrigerator and a microwave. The technician measured the voltage and found it was below the required level. The technician recommended a dedicated circuit and a voltage stabilizer. The machine no longer stopped mid-cycle, and performance improved.
Solving yogur congelado maker performance problems requires a holistic approach. Operators should start with the basics: correct mix formulation, proper pre-chilling, and good cleaning. If the problem persists, they should investigate mechanical and electrical components. Regular maintenance, including cleaning the condenser, checking the drive system, and testing sensors, can prevent most issues. When repair is not cost-effective, replacement or upgrade may be the best option. By choosing a reliable manufacturer such as TAIFAI and following best practices, operators can ensure consistent, high-quality frozen yogurt and minimize downtime.
Final note: Every machine is different. The operator should always consult the manufacturer's manual and seek professional assistance for complex repairs. With proper care, a yogur congelado maker can deliver excellent performance for many years.


